Marine parts must match the conditions around them. Saltwater contains about 33–37 grams of dissolved salts per liter, and shipboard equipment may also face humidity, vibration, temperature changes, or salt-mist exposure. Colvin Friedman supports marine gasket projects by reviewing the application, material, and cutting method before production.
“Marine-grade” does not identify one universal material. EPDM resists UV, ozone, weathering, and heat, but Trelleborg advises against using it with oil products. NBR suits many oil and hydrocarbon applications, but it has different environmental-aging tradeoffs. The right choice depends on the actual fluid, temperature, exposure, compression, and movement.
A gasket must match the joint, material behavior, and installation method. Colvin Friedman reviews fit, function, dimensions, and tolerance during prototyping before production.
Rubber, foam, films, laminates, and adhesive-backed constructions can shift or distort during cutting. Colvin Friedman may use material conditioning, tension control, in-process inspection, and tooling adjustments to manage those risks.
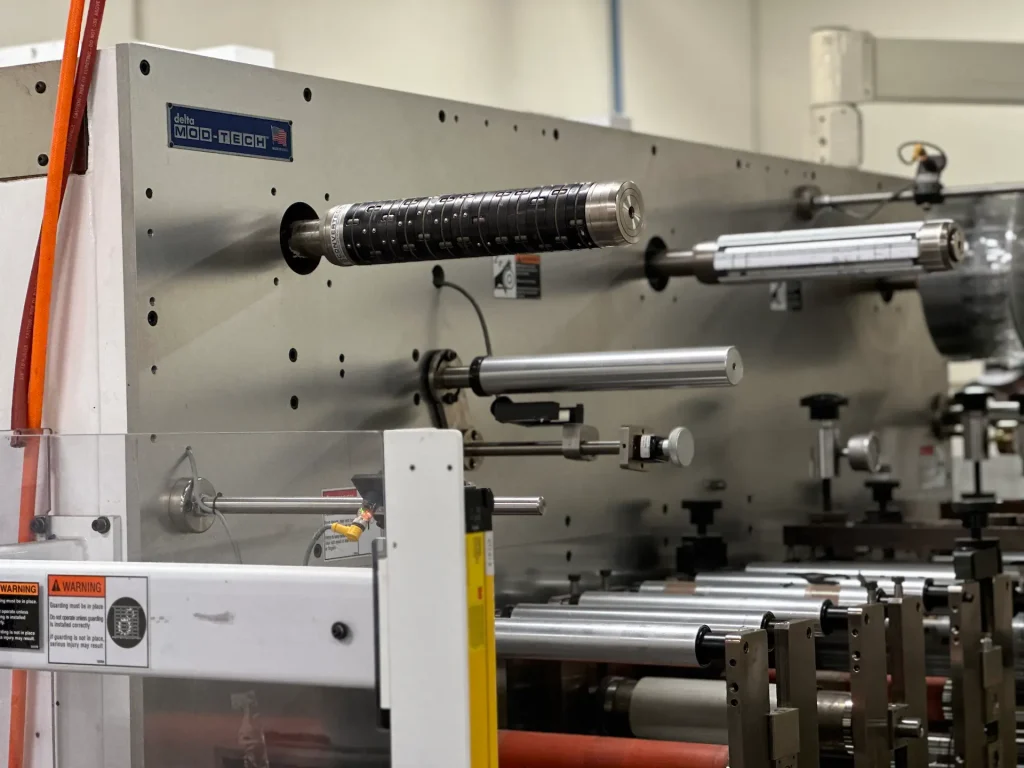
From material selection to final packaging, our die-cutting process is built to deliver reliable marine components that perform in demanding environments.
Share your drawing, sample, material preference, quantity, and service conditions. We evaluate the installation environment, fluid exposure, temperature, compression, movement, and testing requirements.
We choose the best material and die-cutting method based on performance requirements such as moisture, heat, chemical resistance, flexibility, conductivity, and insulation.
Our team designs tooling in CAD, manufactures high-grade steel dies, and produces sample parts for testing and validation.
Prototype parts allow you to verify dimensions and assembly fit before production. We refine the tooling or process if needed.
Equipment is calibrated for your job, and our quality management system monitors production with inspection checkpoints for critical dimensions and cut quality.
Parts are packaged to your specifications, with Kanban and just-in-time (JIT) inventory programs available to support ongoing production.
Ready To Review Your Part?
Send your drawing or sample to confirm material and process fit before production.
The table compares Colvin Friedman’s general rotary and flatbed capabilities. Actual limits depend on the material, geometry, and part size. These figures do not guarantee performance in a specific marine installation.
| Option | Best Fit | Advantages | Limits & Tradeoffs |
|---|---|---|---|
| Rotary Die Cutting | Thin roll-form materials and high-volume production | Published capacity up to 40,000 units/hour, depending on part size. | Maximum thickness is generally 0.015 in. and maximum width is 16 in., both material dependent. |
| Flatbed Die Cutting | Thicker materials, larger parts, or designs requiring a flat press | Handles materials up to 0.5 in. thick and parts up to 40 in. wide (material dependent). | Published capacity is 2,000–4,000 parts/hour, depending on part size. |
Both methods list an average three-week lead time. Published tolerance reaches ±0.005 in. for rotary work and ±0.010 in. for flatbed work, with material-dependent limits.
Colvin Friedman’s marine-specific material identifies neoprene gasket applications for boat hulls and engine compartments. It also lists deck hardware and marine equipment that needs weather protection. The source does not establish a universal rating for every neoprene compound or marine installation.
Colvin Friedman combines rotary and flatbed die cutting with material review, CAD tooling, prototyping, inspection, packaging, and stocking support. Its company materials identify U.S.-based production in Petaluma, California, plus direct technical access to Vice President Josh Rodman.
Start with a design review. Send a drawing or sample when available. Add the part number, material, quantity, tolerance, adhesive requirement, and service conditions if you have them. The quote form accepts an uploaded drawing, part number, material type, quantity, and comments.
Yes. Provide the actual fluids, temperature range, exposure, compression, and movement. The team can review material options, but final qualification remains specific to the part and assembly.
Rotary cutting generally suits thin roll materials and high-volume production. Flatbed cutting generally suits thicker materials, larger parts, or designs that need a flat press. The team reviews the material, geometry, tolerance, and quantity before recommending a method.
Yes. Colvin Friedman’s process includes prototype parts and fit-and-function testing before full production.
Include a drawing or sample when available. Add the part number, material, quantity, and comments about the application. Supplemental details about fluids, temperature, compression, adhesive, or tolerance can help the team review the project.
The available information does not establish a blanket marine certification. Confirm the documentation and testing required for the specific part, assembly, vessel system, or governing standard.
Send your drawing, sample, or part details to discuss material selection and process fit. Colvin Friedman can review your marine application and prepare a quote.