
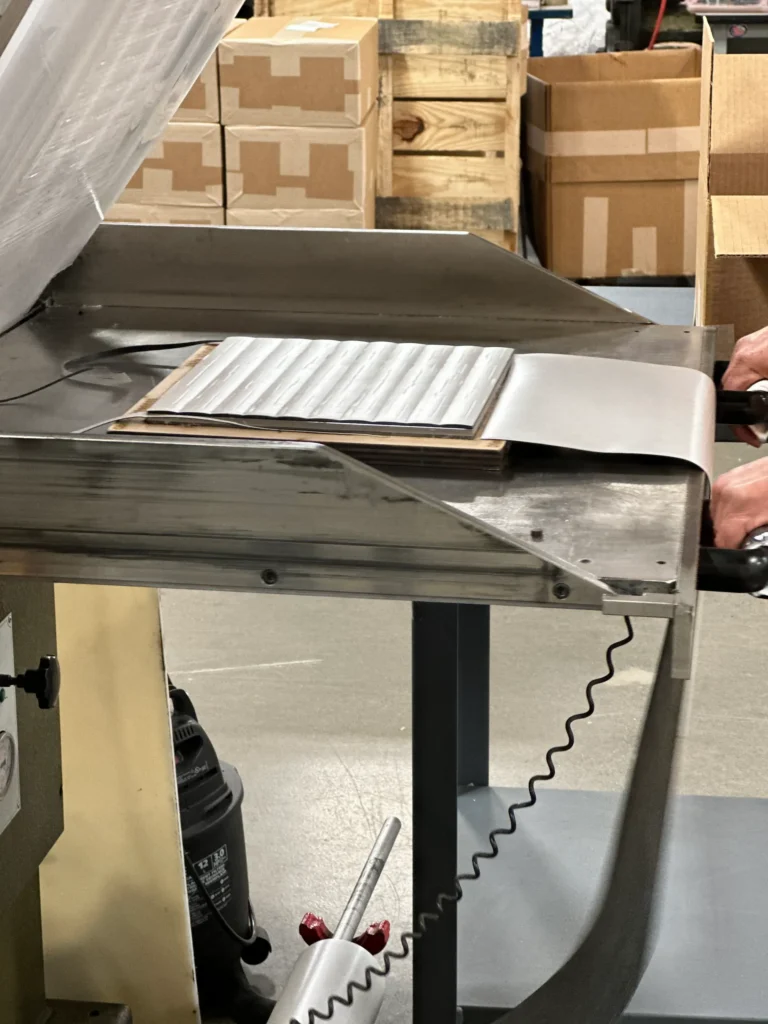
Rotary die cutting uses a rotating cylindrical die and anvil roll to cut, perforate, crease, or kiss-cut material as it moves continuously through a press. Because the material feeds through the machine without stopping between cuts, the process supports fast, consistent production across high-volume runs.
Rotary die cutting also works well for parts that require tight repeatability, intricate shapes, or multiple features within the same design. It is commonly used for flexible materials supplied in rolls, including films, foams, adhesives, plastics, and other thin substrates.
What You’ll Learn:
The Five Steps of Rotary Die Cutting
A rotary press moves roll-fed material, known as the web, through several stages in one continuous pass. Each stage keeps the material aligned, controls the cut, and prepares the finished parts for use.
Flexible vs. Solid Rotary Dies
Rotary presses use one of two die types. Material thickness and run length decide which type fits the job.
| Die Type | Flexible Die | Solid Die |
|---|---|---|
| Construction | Thin engraved steel wrapped around a magnetic cylinder | Cutting pattern engraved directly into the cylinder |
| Best for | Shallow or partial cuts, lower-pressure jobs | Deep cuts through thick or multilayer material |
| Tooling cost | Lower | Higher |
| Durability | Lower; the steel sheet replaces easily | Higher; the cylinder can be resharpened |
Flexible dies also need minimal downtime to swap, since the cutting sheet mounts onto the outside of the cylinder rather than being machined into it.
Types of Rotary Presses
Rotary presses can differ by drive system and web width, while features such as in-register cutting, slitting, and roll-to-roll processing can be added based on the part and production setup.
Servo-Driven Rotary Presses
Servo-driven presses give individual stations independent, computer-controlled movement. This allows for finer registration and tighter control when parts require multiple layers, printed alignment, or more complex processing.
Line-Driven Rotary Presses
Line-driven presses connect multiple stations through a shared mechanical drive shaft. They use a simpler setup than servo-driven systems and can be a practical option for straightforward, repeatable production runs.
Narrow-Web Rotary Presses
Narrow-web presses are designed for smaller roll widths and are commonly used for compact parts, labels, adhesive components, and other precision-cut pieces.
Wide-Web Rotary Presses
Wide-web presses handle broader material rolls, making them better suited for larger parts, wider sheets, or layouts that place multiple part lanes across the web.
Inline Rotary Press Capabilities
Depending on the press configuration, manufacturers can also:
Rotary vs. Flatbed Die Cutting
Rotary and flatbed die cutting can produce many of the same types of parts, but they handle material and production volume differently. Rotary presses keep material moving continuously through the machine, while flatbed presses stop and reposition the material for each cut. That difference affects speed, material thickness, tooling cost, and the types of jobs each process handles best.
When Rotary Die Cutting Makes More Sense
Rotary die cutting works best for high-volume runs using thin, flexible materials. Because the web moves continuously, a rotary press can produce parts much faster than a flatbed press and maintain tighter tolerances across long production runs.
It is especially useful when:
- Production volume is high.
- Material is thin and roll-fed.
- Tight repeatability is important.
- Parts need to align with printed or laminated layers.
- The same die will be reused for future orders.
When Flatbed Die Cutting Makes More Sense
Flatbed die cutting is better suited for thicker or more rigid materials and lower-volume production. The press stops for each cut, which slows production but allows it to handle materials and part sizes that may not work on a rotary press.
Flatbed can also make more sense for shorter runs because tooling typically costs less upfront.
How the Two Compare
| Factor | Rotary | Flatbed |
|---|---|---|
| Material Thickness | Up to 0.015 in | Up to 0.5 in |
| Production Speed | Up to 40,000 units/hour | 2,000–4,000 parts/hour |
| Tolerance | ±0.005 in | ±0.010 in |
| Tooling Cost | 500–2,000 | 100–500 |
The right method usually comes down to material, volume, and part requirements. Rotary die cutting favors speed and repeatability at scale, while flatbed die cutting offers more flexibility for thicker materials and shorter runs.
Materials, Cut Types, and Finished Parts
A rotary press processes many roll-fed materials in a single pass.
| Material Category | Examples |
|---|---|
| Plastics | Polyester film, PET, vinyl, acrylic |
| Foams | Polyurethane, EVA, polyethylene, neoprene |
| Adhesives | Single- and double-sided tapes |
| Metals | Thin-gauge aluminum, copper, stainless steel foil |
| Rubbers | EPDM, silicone, neoprene, natural rubber |
| Other | Paper, fabric, felt, nonwovens, composites |
Within a single pass, a rotary press can also kiss-cut material (cutting through the top layer only and leaving the liner intact, so labels and similar parts peel away cleanly), perforate it for tear lines, crease it for fold lines, or cut metal-to-metal for parts that need a clean edge through every layer.
Common finished parts include:
- Lenses cut for consistent edge quality
- Gaskets and seals cut to a uniform thickness for a reliable seal
- Decorative leather cut into repeatable shapes
- Shims cut to tight thickness tolerances
- Face shields cut and shaped for face and eye protection
Many of these parts combine multiple material layers laminated together during the same pass. Rotary die cutting projects typically move from design to first parts in about three weeks, whether the order calls for prototype quantities or millions of parts. Most of that time goes into building the die itself, since production can start as soon as the die is mounted and set.
Industries That Specify Rotary Die Cutting
Rotary die cutting is widely used in industries that need high volumes of consistent parts made from thin, flexible materials.
- Medical Devices and Wound Care: Used for gaskets, pads, dressings, and adhesive components where consistent dimensions support proper fit and performance.
- Automotive and Marine: Common for trim, seals, insulation, and adhesive-backed parts that need repeatable shapes across large production runs.
- Electrical and Energy Equipment: Used for insulation, shielding, spacers, and other components that help protect or separate parts within an assembly.
- Construction and Defense: Supports repeat production of gaskets, seals, insulation, and protective components made to specific material requirements.
- Pharmaceutical Packaging: Helps cut, perforate, and shape packaging materials quickly while maintaining consistent placement and dimensions.
Find the Right Die Cutting Process for Your Part
Rotary die cutting can improve speed, consistency, and repeatability when the material, tooling, and press setup match the application. If you are planning a high-volume run or comparing rotary with another cutting method, learn more about rotary die cutting services and talk with the Colvin Friedman team about the right approach for your part.