
Precision-cut Kapton®, Nomex®, PET, and 20+ dielectric substrates: from prototype to full-volume production, with zero recorded quality rejections.
Your insulators need to hold spec across every run, not just the prototype. Colvin-Friedman has cut precision electrical insulators since the 1950s. We work directly with your engineering team, hold ±0.005″ on thin films, and ship prototypes in days. Every job is custom. No catalog. No guessing.
Or call Josh at (707) 769-4488
| Material | Temperature Range | Key Properties | Common Applications |
|---|---|---|---|
| Kapton® Polyimide | –269°C to +260°C | 7,700 V/mil dielectric strength; chemical resistant | Transformer tape, motor slot liners, aerospace wiring, flexible heaters |
| PET (Mylar®) | –70°C to +150°C | Dimensional stability; cost-effective | Circuit boards, battery separators, capacitor film |
| Nomex® Aramid | Continuous to +220°C | High dielectric strength; Class B–F insulation | Motor phase barriers, transformer winding insulation |
| PVC Film | –10°C to +105°C | Flame-retardant, flexible, printable | Cable insulation, electrical labels, protective sleeves |
| G10/FR4 Epoxyglass | Continuous to +130°C | High mechanical strength; flame-retardant | High-voltage bushings, circuit board substrates |
| Fish Paper | Up to +105°C | Electrically insulating; heat-resistant | Fuse tubes, motor slot insulation, device barriers |
Need a material not listed? Send us your spec; we source custom substrates for specific applications.
From prototyping through high-volume production, every run is engineered for consistent quality, assembly readiness, and supply-chain reliability.
±0.005" on rotary-cut films and ±0.010" on flatbed substrates across full production runs.
Burr-free insulators designed to keep coil insertion and SMT lines running without rework.
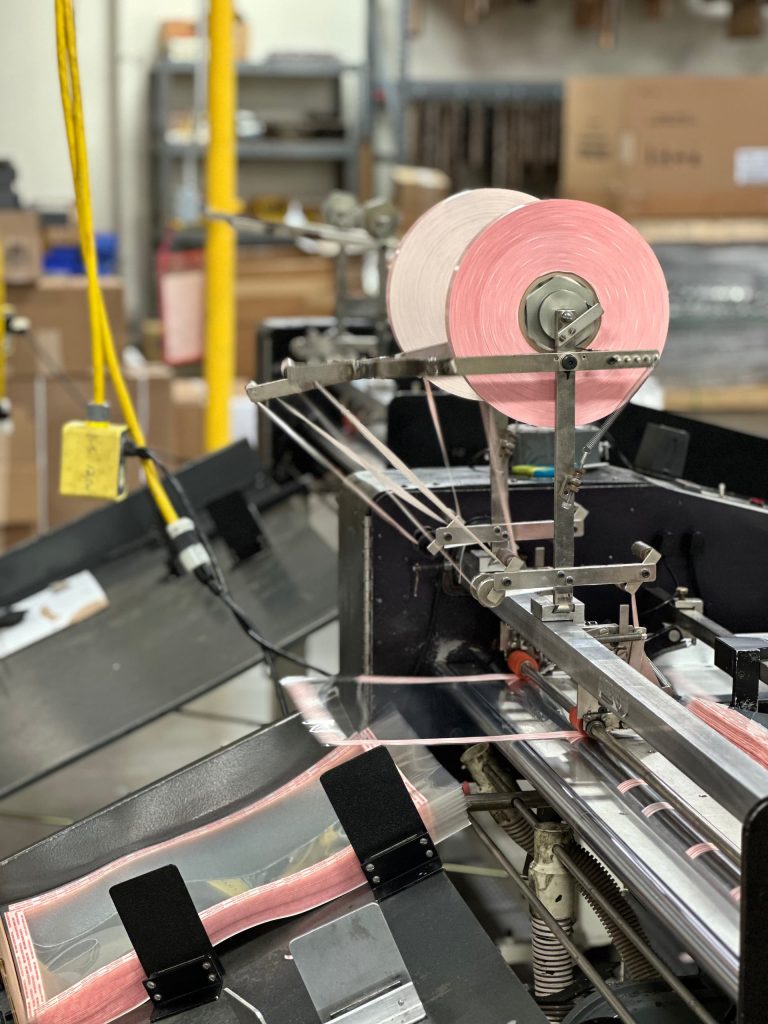
Insulator is cut while the release liner stays intact for easy peel-and-place assembly.
Multi-cavity tooling produces intricate slots, apertures, and shapes in a single pass.
Industrial-grade 3M and Adhesives Research tapes laminated inline with no extra handling.
Up to 40,000 units/hour while maintaining specifications through QMS checkpoints.
Prototype specifications transfer directly into production tooling without repeated handoffs.
Kanban and JIT support with automated replenishment to help prevent stock-outs.
Accepts DXF, DWG, PDF, or hand sketches and provides production-ready CAD for approval.
Or call Josh at (707) 769-4488
You work directly with Josh Rodman, our Vice President, for same-day technical support and production oversight, backed by more than 70 years of expertise in materials and tooling. Our California facility ships prototypes in 3–5 business days, with custom-only production built to your drawings and the same engineering attention for every run. We maintain a zero record of quality rejections, and our engineers identify tolerance, radius, and adhesive issues before tooling is cut, helping you avoid rework, delays, and line shutdowns.
Or call Josh at (707) 769-4488
| Category | Colvin-Friedman | Large Converters | Overseas Suppliers |
|---|---|---|---|
| Communication | Direct to VP Josh Rodman | Through account managers | Email only; time-zone delays |
| Lead Time | Prototypes in 3–5 days | 1–3 weeks | 4–8 weeks + shipping |
| Material Range | 20+ electrical substrates from one source | Often specialized | Limited options |
| Quality Track Record | Zero recorded rejections | Varies by facility | Inconsistent |
| Custom Engineering | Co-engineering from sketch to production | RFQ-based; limited DFM | Minimal |
| Supply Chain | Kanban/JIT; 99.99% stock-out avoidance | Standard fulfillment | Large MOQs; long cycles |
Or call Josh at (707) 769-4488
From initial drawing to final delivery, our five-step process keeps engineering, tooling, production, and quality control aligned, reducing delays and avoiding costly changes late in the process.
01
Engineers review your drawing, confirm materials and lamination needs, and flag potential issues before tooling.
02
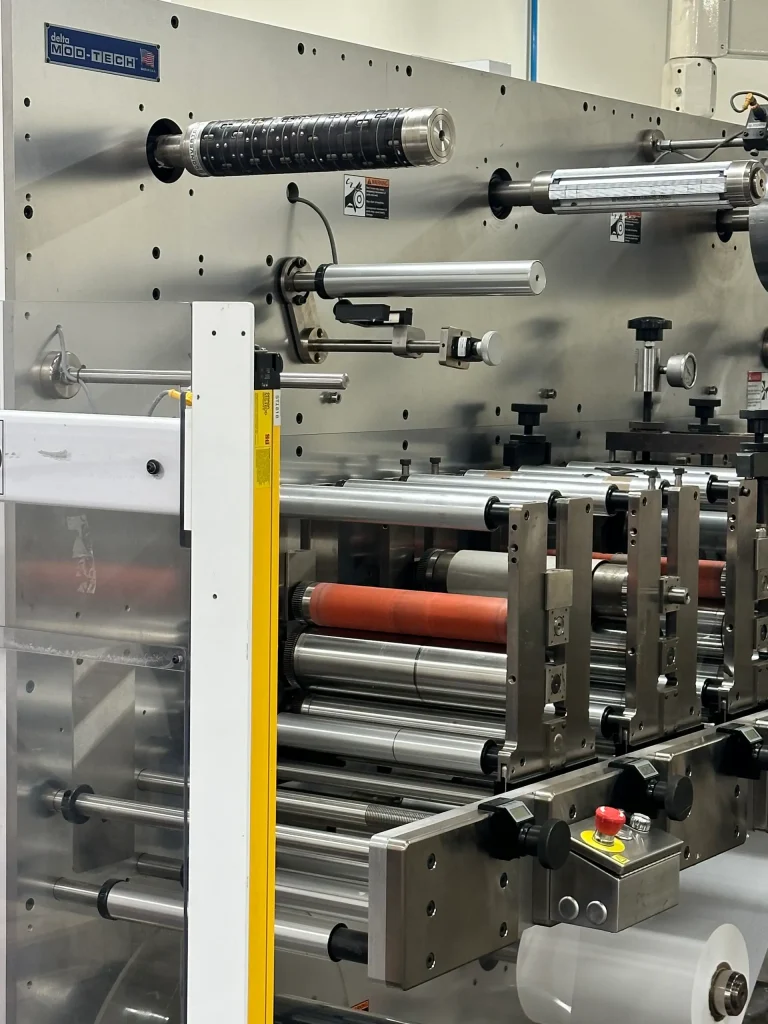
High-grade steel tooling is milled, heat-treated for edge retention, and tested before production.

03
Fit-and-function samples are shipped for validation, allowing adjustments before full production.
04
CAM-driven presses scale to volume with QMS checkpoints and inline lamination.
05
Parts are inspected, packed as rolls, sheets, or kits, and integrated into your Kanban or JIT pipeline.
Kapton® and PET films curl under poor tension control. We set cut conditions to each material's actual stress response.
Depth, adhesive mass, and vacuum hold-down are dialed in during setup, not discovered during a bad run.
Tight radii, tiny through-holes, and adhesive tab placement get flagged at CAD review, not after first articles fail.
Press operators make live adjustments to pressure and blade clearance before tolerance drift becomes a defect.
UL 94 flame ratings, AS9100 for aerospace, and RoHS for European markets are available. Tell us your requirements before quoting.
We work with your preferred supplier. Confirm during the quoting phase.
A drawing with dimensions and tolerances, material type and thickness, and estimated annual volume. Note any lamination, certification, or finishing requirements.
| Metric | Result |
|---|---|
| OEM Production Quality Rejections | Zero recorded |
| Rotary Press Throughput | Up to 40,000 units/hour |
| 0.001″ Kapton® Tolerance | ±0.005″ across full production |
| Prototype Turnaround | 3–5 business days |
| Production Tooling Lead Time | 2–7 days |
| Stock-Out Avoidance Rate | 99.99% |
| Electrical Insulation Experience | 70+ years |
Our precision-cut electrical insulation materials support demanding applications across electronics, e-mobility, power, motor, generator, and battery manufacturing.
EMI/RFI shields, thermal-transfer pads, transformer sleeves, and battery-cell spacers in polyimide and PET; ±0.005" tolerance and burr-free for SMT.
Nomex® and Kapton® phase barriers, slot liners, and winding insulation; G10/FR4 bushings cut on flatbed without cracking.
Slot liners, phase insulators, and wedge stock in polyester film, aramid paper, and DMD composite; burr-free for automated coil insertion.
Cell spacers, electrode masks, and terminal insulators from flame-retardant, thermally resistant polyimide to help prevent thermal runaway.
Not sure if your application fits? Send us the spec. Josh responds within one business day.
Or call Josh at (707) 769-4488
±0.005″ on rotary-cut Kapton® as thin as 0.001″. Flatbed holds ±0.010″ on thicker substrates. We review your drawing and recommend the right configuration before quoting.
Yes. We offer inline PSA lamination using 3M and Adhesives Research tapes. Kiss-cutting leaves the liner intact for peel-and-stick assembly.
Prototypes ship in 3–5 business days. Production tooling takes 2–7 days, then ramps to volume. No overseas freight delays.
Yes. Up to 40,000 units/hour on rotary presses, with Kanban/JIT integration and 99.99% stock-out avoidance.
DXF and DWG files work. So does a PDF or a hand sketch. We return a production-ready CAD drawing for approval before any tools are made.
Yes. Tell us during quoting, and we confirm compatibility before production starts.
Send us your drawing, material specs, and volume requirements. Josh Rodman responds within one business day with accurate pricing and lead times.
Call Josh directly: (707) 769-4488