
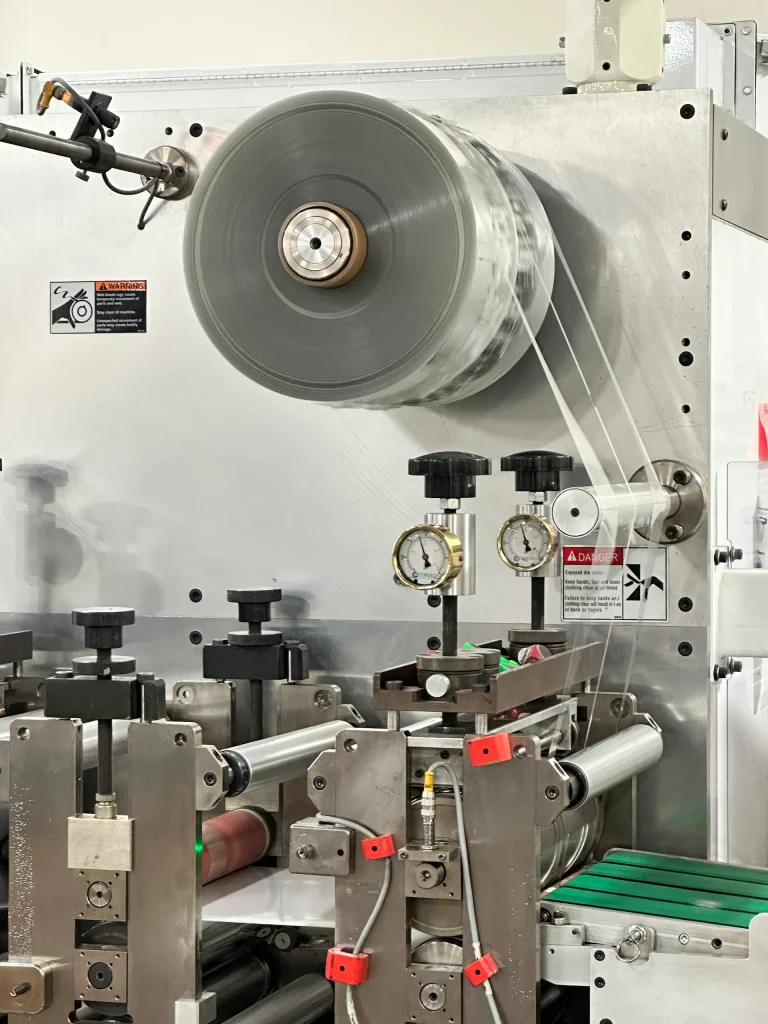
A flatbed press pushes a custom die through sheet material in one controlled stroke. The press stops between cycles, so it can handle thicker, more rigid substrates than a rotary press can run.
This guide covers:
How Flatbed Die Cutting Works
A flatbed press holds the material flat while a die drops onto it under hydraulic force. The die cuts, creases, or perforates the sheet in a single pass, then lifts clear so the operator can move to the next section.
Die shops build flatbed dies in three ways, and the die type affects both cost and turnaround. The table below breaks down each option.
| Die Type | Tooling Cost | Best For |
|---|---|---|
| Steel rule | $100 to $500 | New designs, prototypes, and lower-volume runs |
| Forged | Higher, project-dependent | Long production runs that need a durable, resharpenable die |
| Etched | Project-dependent | Fine or delicate patterns a stamped blade cannot hold |
Every run starts with a first-article check before full production begins. A quality management system verifies tolerance, dimensions, and fit against the print, then runs a functional fit test to confirm the part performs as designed. If a measurement drifts outside spec, the operator adjusts die pressure or alignment before the press continues.
Material Thickness and Tolerance Capabilities
Flatbed presses run the thicker, more rigid materials that rotary presses cannot process. The table below lists the specifications a flatbed press typically holds, followed by the material categories that fit those specifications.
| Specification | Flatbed Capability |
|---|---|
| Max material width | 40 inches |
| Max material thickness | 0.5 inches |
| Tolerance | ±0.010 inches |
| Production output | 2,000 to 4,000 parts per hour |
| Tooling cost | $100 to $500 |
| Material | Common Examples |
|---|---|
| Plastics | PET, PVC, polycarbonate (thick sheets) |
| Rubber | Neoprene, EPDM, silicone |
| Foam | Closed-cell and open-cell foam padding |
| Composites | Rigid laminates and fiberglass |
| Metal foil | Aluminum and copper over 0.015 inches |
Flatbed vs. Rotary Die Cutting
Rotary die cutting moves material continuously past a rotating die and anvil. It fits thin, flexible substrates that run at high volume. Flatbed die cutting stops the material between strokes instead, so it fits thicker or more rigid substrates and shorter runs. The table below compares the two processes directly.
| Specification | Flatbed | Rotary |
|---|---|---|
| Max width | 40 inches | 16 inches |
| Max thickness | 0.5 inches | 0.015 inches |
| Tolerance | ±0.010 inches | ±0.005 inches |
| Output | 2,000–4,000 parts/hour | Up to 40,000 units/hour |
| Tooling cost | $100–$500 | $500–$2,000 |
A thin film or foam under 0.015 inches runs faster and cheaper on a rotary press. A rigid composite, thick rubber sheet, or metal foil above that thickness needs a flatbed press instead. Flatbed tooling also costs less to build and swap, so it fits projects that expect design changes or run in smaller batches.
The crossover point between the two processes usually falls in the thousands of units, not the hundreds or the hundred-thousands. Below that volume, flatbed’s lower tooling cost outweighs rotary’s speed advantage. Above it, rotary’s per-part savings outweigh the higher tooling investment, provided the material and design stay stable enough to justify it.
Industries and Applications
Manufacturers across several industries specify flatbed-cut parts when the application carries tight tolerances or uses dense materials.
| Industry | Common Flatbed Applications |
|---|---|
| Aerospace and Defense | Thermal insulation, vibration dampeners, gaskets built to aerospace-grade tolerances |
| Medical Devices | Die-cut adhesives, electrode pads, gaskets with QMS traceability |
| Electronics | EMI shielding, thermal management films, RFID barriers |
| Automotive | Gaskets, seals, interior components, sound-dampening materials |
| Energy | High-pressure seals, gaskets, battery thermal management films |
When to Choose Flatbed Die Cutting
Choose flatbed die cutting when a project meets one or more of these conditions.
- The material runs thicker than 0.015 inches or resists rotary tooling.
- The design still changes between runs.
- The order fits a short- to medium-run production need rather than a continuous, high-volume order.
- The part needs a die that costs less to build and modify.
Lead time rarely factors into the decision. Both processes run on a similar production schedule, so the material, tolerance, and run length should drive the choice, not turnaround time. A thin, flexible substrate at high volume usually runs faster and cheaper on a rotary press instead.
Further Reading
- Flatbed vs. Rotary Die Cutting: How to Make the Right Choice for Your Next Project
- The Complete Rotary Die Cutting Process Explained
- Standard Die Cutting Tolerances: Complete Guide
- Die Cutting Materials Guide
Start Your Flatbed Die-Cutting Project
Colvin-Friedman handles flatbed die-cutting projects for thicker, rigid, and specialty materials that need controlled cuts and consistent tolerances. With decades of die-cutting experience, the team can match tooling, press setup, and production requirements to your part specifications. Talk to Colvin-Friedman about your flatbed die-cutting project.